PUBLICATION
Lean manufacturing: intrigue or intriguing?
Lean manufacturing and management has become one of the best competitive strategies in this century. But is the implementation of ‘lean’ as simple as thought by many companies? Is following lean tools the key to success? Let’s find out with the example of manufacturing practices in Boeing factory…
Becoming lean or transforming an organisation to become ‘real’ lean is not difficult. That has been my experience over the past two plus decades so far. Why then many organisations struggle with the process and fall short of becoming a truly lean company? What makes companies attempt sporadic implementation with a few tools at random and live in the wonderland of misconception that they too are a lean organisation? Using a dozen tools and structuring a production system with measurements, keys, score cards, rating by copying similar attempts does not make a ‘true’ lean company. Such companies who wish for lean results are dominated by short term thinking. If Toyota uses over ninety tools, how many do you think are known outside Toyota? Alix Partners of New York found that of the surveyed one hundred companies who had embarked on their lean journey, over 95% could not get expected results, while only half the remainder are making progress. Why?
What is lean?
Lean manufacturing principles are ostentated by companies as an effective way to eliminate waste and boost the bottomline and yet many often do not achieve decent levels of productivity or savings. Lean principles have grown in popularity over the past four decades after Toyota showed lean thinking as a key driver of continuous improvement and not just cost cutting. Most companies don’t apply lean principles in a way that gives them and their customers the maximum benefits. Many view lean implementation as a checklist of do’s and don’ts as a part of their business process rather than a broader way to run an entire company.
Lean manufacturing philosophies can lead to significant change. Companies must be cautious not to throw out the principles as some fail to implement them correctly. Lean success stories tell us that where lean programmes are properly executed, long-term all-round benefits have been substantial. Managements must view long-term cultural change as their topmost priority, to get the maximum results. Such change is also essential if lean benefits are to be sustained.
“Lean is a manufacturing philosophy that shortens the timeline between customer order and shipment by eliminating waste”, John Shook. This does not mean that we keep a large amount of inventory and ship as & when we get an order. But it means that we build what the customer orders as soon as possible, after the order has been received and the total lead time is as short as possible. When a product sits in a queue anywhere anytime – it is a waste. Building a product and its parts in a one piece flow, in a levelled and mixed production sequence is vastly superior to large ‘batch and queue’ production.
Lean production is ‘lean’ because it uses less of everything (human effort, space, investment, development time, etc) as compared to the batch or mass production. It facilitates in creating a flowing inventory rather than stationary, resulting in very little inventory stocks, therefore, fewer defects and can produce a greater variety of products.
Ways of thinking
The concepts of ‘batch or mass production’ and ‘lean production or lean manufacturing’ do not refer to production systems. They reflect the ‘ways of thinking’ about production. They are the assumptions that underline how people and institutions formulate solutions to problems of organising people, equipment, material and capital to create & deliver products to customers. Batch or mass and lean are thus paradigms that reflect and inform the thinking about production within different eras and their cultures.
For most part of the twentieth century, the original Ford production system and all systems subsequently developed by the auto industry and copied by rest of the manufacturing world reflects the mass paradigm. The rise of the Japanese manufacturing took place after WW-II within the constraints of effective operations in mass paradigm, giving birth to a new approach to manufacturing that today we call lean manufacturing – best exemplified by Toyota Production System (TPS). Hence, TPS is nothing more or less than a set of solutions designed to achieve the lean ideal.
Lean manufacturing includes a set of techniques that comprise a system that are derived from a philosophy. The benefits of lean will accrue if understanding and implementation is accordingly. TPS is a system, not a set of isolated practices. Some of its fundamental principles fly in the face of common sense batch or mass production thinking. Everybody wants to build in quality, so they need reliable equipment. Nobody wants a messy disorganised shop floor. But focusing on quality, machine reliability/TPM/OEE, Kanban, workplace organisation and visual factory (5S), does not get us continuous flow, pull and striving for excellence.
The batch or mass production thinking is incapable of understanding why we shut down a machine after just enough production has been made, or why we would like to eliminate the safety stocks, or why we might prefer to use number of smaller machines dedicated to separate product lines rather than one machine that provides economies of scale, or why we would change over a machine several times in a shift instead of running one product through the shift to improve the equipment utilisation.
Becoming lean
To become a lean manufacturer requires the elements of flow, pull & strive for excellence. It requires a way of thinking that focuses on making the product flow through the value stream without interruption; a pull system that cascades back from customer demand by replenishing what the next operation takes away at short intervals; and a culture in which everyone is striving continuously to improve. It’s quite simple! But, is it that simple in practical? The answer may be ‘no’. This is where a Sensei can help you.
Employees of lean companies participate in problem-solving through quality circles. While true lean companies build in quality rather than inspect it after the occurrence. Quality consultants may have made hay teaching SQC methods and problem-solving techniques. Although true lean companies focus on customer, quality alone will not be enough as we cannot stop at competing on quality; we must also compete on cost, on-time delivery and service.
Where there is trouble in conceptually understanding lean manufacturing, there is more difficulty in implementation. Most of the concepts are simple, many are common sense and others are counterintuitive. Many would claim to understand more or less how we need to change the way we run our plants, but still struggle to make it happen. Some problems that continue to be visible are:
- The way manufacturing works with sales makes scheduling and running the plants difficult. In some companies, the way sales works with manufacturing makes their manufacturing discrete.
- The above is compounded by the way we order material from suppliers.
- Labour and management still don’t trust each other.
- The way we measure performances doesn’t provide information useful to run a plant and may encourage wrong decisions.
- In many places, the equipment is designed for the old paradigm, combined in layouts that seek economies of scale, singing ‘bigger is better.’
- Senior management is reluctant to get involved and take charge of the lean implementation.
Becoming lean is to focus on reducing non-value added wastes; where waste is anything that impedes the flow of product as it is being transformed in the value chain. This means getting the product where it is needed, when it is needed and in the exact quantities needed. Inventory buffers, quality problems and time spent in transit are all impediments to flow. Only when we drive out the non-value added wastes continuously, will we begin the lean journey.
Lean manufacturing is perhaps the best competitive strategy companies can implement to gain competitive advantage. Toyota has demonstrated this many times, from the oil crisis of the 1970’s to the recent brake pedal floor mat issue of 2011. Every time they have come out stronger and better. Likewise, Mysore Kirloskar demonstrated how lean thinking could be used to turnaround a company from closure. Bridgeport’s JV in Indonesia demonstrated how after five years of losses, lean thinking could turn its fortunes!
Recently, I had visited the Boeing factory that spreads over 1,010 acres of land attached to the Paine Field runway (longest in the world). Applying lean thinking has enabled them to assemble a Boeing 747 in three days. Surely, this is a huge change from 1970 or 1989 when the Boeing 747-400 entered the market. Beginning to learn from TPS in the 1990’s and implementing the concepts has created this change. The newer versions like Boeing 777 and the Dreamliner Boeing 787 are presently assembled in four days, and by 2014 they will bring assembling time down to three days. The Boeing 747 uses about six million parts, while the Boeing 777 uses half the number, and Boeing 787 even less; perhaps using the tools of design, standardisation and rationalisation. The Boeing 777 is a long haul aircraft; which was test flown non-stop for 22 hours and 42 minutes! It’s little surprise that the Dubai Air Show awarded it orders worth USD 100 billion. Better, faster, safer and farther is the way to go for the airline industry.
Culture
Lean is a way of life; therefore it is about culture and not about tools. Culture is what the leadership builds. Lean is a way of thinking about value and adding value. Lean is an evolution; therefore it is about innovation, ideas and solving problems. Lean is as imagined through TPS, although I am open to new ideas, I don’t think there is scope for non-lean companies to re-imagine lean their way. I believe that true lean companies are constantly attempting to make it better, faster and cheaper.
Speaking recently in the USA, I was asked many questions on how we build the lean culture. They all understand the tools. Tools are almost a no-brainer, although they are used to solve problems. Building culture is another ball game. That’s why when Toyota Sensei once said, “I can teach you everything, but you still can’t do it.” He was defining the distinction between leading change and wishing it to happen.
It takes a committed, dedicated and dynamic leadership to transform an organisation to become true lean. It involves leadership modifying their daily routine to fall in compliance with the implementation process. This includes learning, experimenting, practicing and training others. It involves spending the required time on the Gemba (shop floor). Change requires to be led in every activity by doing (body language) and not by lip service. People look at what you do and not at what you say. The old maxim of ‘monkey see, monkey do’ still works. Companies don’t succeed, people do; people don’t succeed, their attitudes do! Succeeding with lean is about bringing those required attitudes to surface and putting in some relentless work. Get a good Sensei who’s been where you want to go, and he can help. After all, there is no gold medal to win in lean; everyone who stays the course and goes the distance wins!
Download the original PDF Lean-Manufacturing-intrigue-or-intriguing.pdf
Download PDF ↓ Originally published in Efficient Manufacturing · January–February 2014
Keep reading
More on Lean Manufacturing
ARTICLE
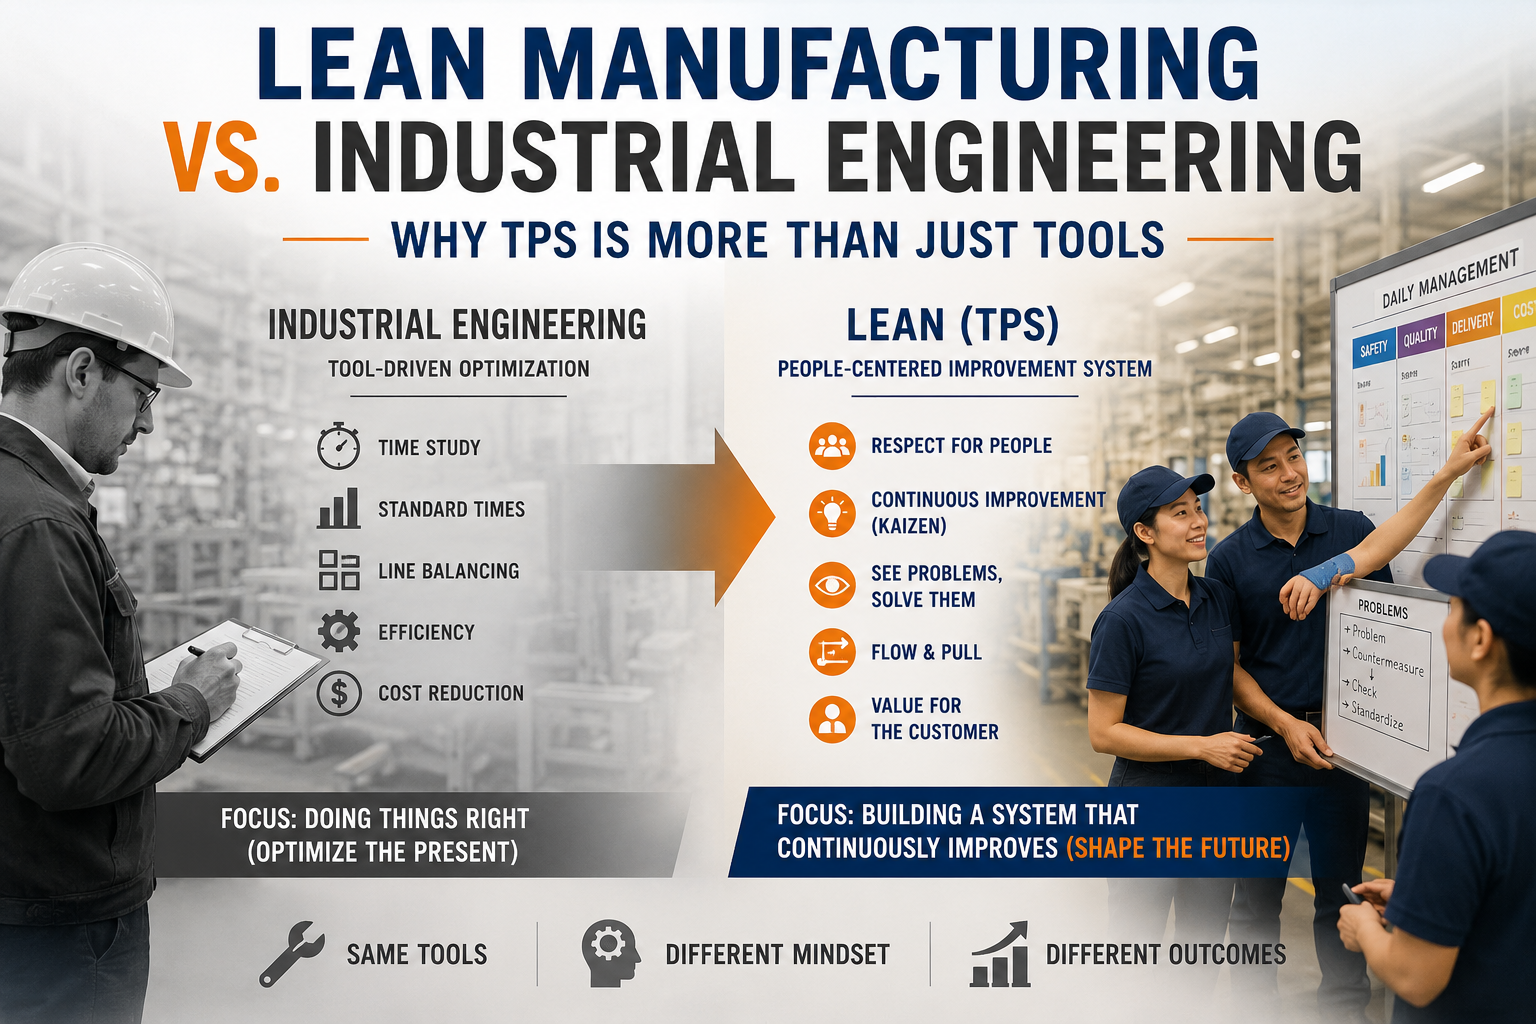
Lean Manufacturing vs. Industrial Engineering: Why TPS Is More Than a Toolkit
Lean ManufacturingMay 2026