PUBLICATION
Lean's the way
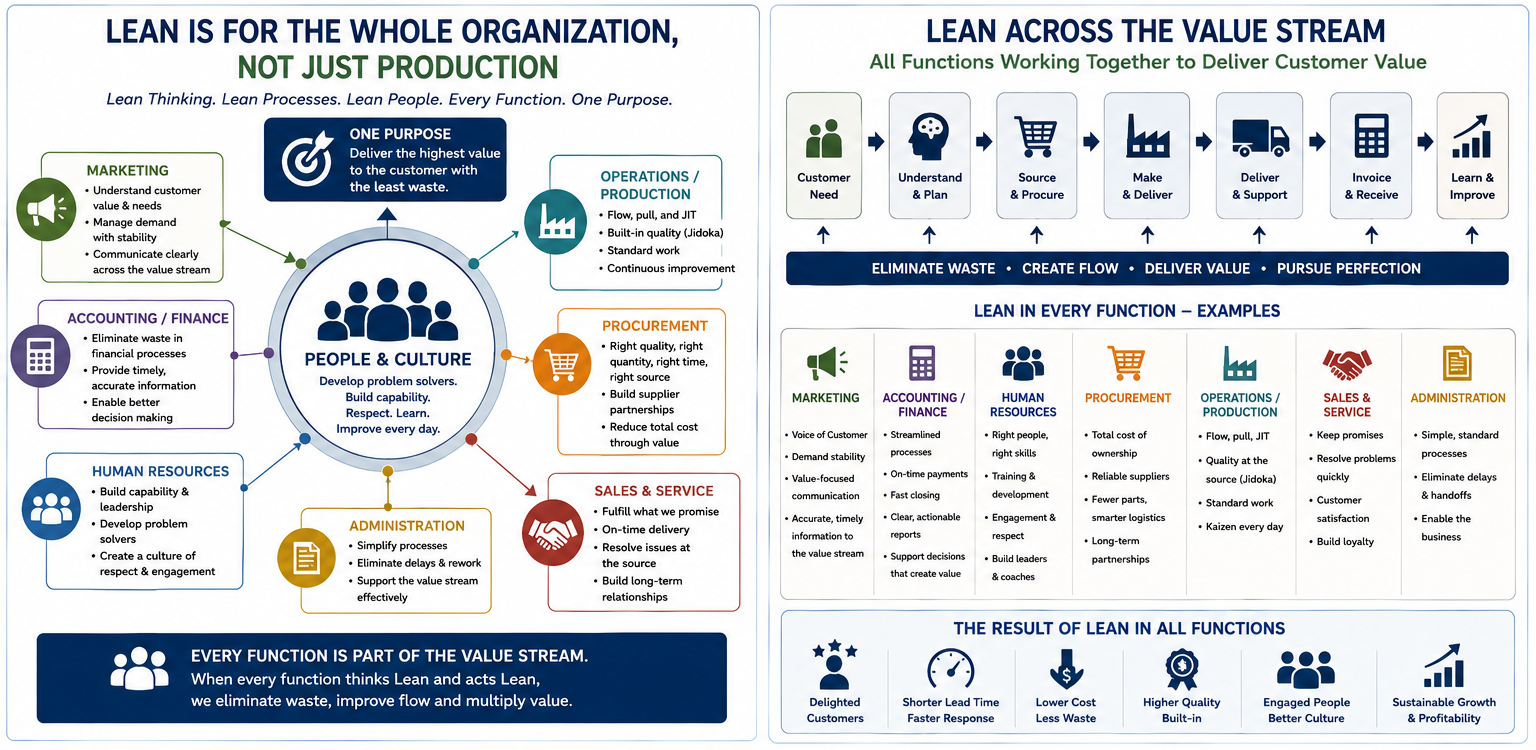
Lean manufacturing allows manufacturers to be fast and nimble enough to quickly react to changes in customer demand and do it with little inventory. In these changed times, lean supply chain performance must be the goal of every manufacturer. Creating the lean supply chain by streamlining business and production processes to significantly reduce cycle time, decrease inventories, lower costs, and increase customer service, has become the mandate for gaining competitive advantage.
“Companies don’t succeed, but people do.” Making products is about making people. Developing a production system and developing people cannot be separated, they are integral if you want to succeed in the long run.
Mysore Kirloskar (MKL) had two factories, headquartered in Harihar, with Hubli housing the other plant. At the beginning of the 1990s, we at MKL were implementing the just-in-time (JIT) techniques at the Hubli factory, and so we belonged to the demi-monde that was an exemplum to many companies who then visited us to study about the implementation of JIT techniques and discuss the problems and difficulties faced by them in their attempt to do the same. In our system of operation at MKL then, broader corporate policies were routed to us through Harihar. And while implementing the lean manufacturing system at MKL Hubli, we had to face many communications and policies of the company that conflicted with our lean thinking and strategies. Why did we have such a situation where some directives clashed with the lean culture, where normally should not have been? One, it was because one factory was transforming to becoming lean while the other continued to be discrete. These are two different cultures. The other probably being that, after Dr Schonberger set us on our journey we had no Sensei to guide and assist us, who may have helped in permeating better understanding thereby helping to regulate the policies better.
One such communication at MKL was in our human resource development policy that said we categorise all employees into categories – A, B and C. Using the normal distribution curve, chances were that there would be about 10 per cent of employees in the C category who should be allowed to go every year. Obviously, whoever had prompted such a policy had read about it from a Jack Welch interview. On the other hand we at Hubli were doing our best to train the people, develop their skills and abilities that would help them perform their jobs with distinction, which in turn would benefit the organisation. This differentiation would have only demoralised the workforce and we would have triggered them thinking, ‘who is next?’ But we would overlook our responsibility of developing them to their best potential. We were doing our best to help them develop their skills and abilities, while they were responsible to make their best effort. Working on the premise that ‘if the student hasn’t learnt, the teacher hasn’t taught,’ we not only trained but tried to find the best possible jobs for the slow learners. We created an environment where hardworking people would thrive and be supported while the ones with the wrong attitude would be allowed to go. We at MKL believed that it is necessary to work hard to identify the critical knowledge about the work, and find ways to transfer that knowledge and achieve significant performance levels. In your effort to achieve excellence and respond to tomorrow’s customers, perhaps a challenging thought would be ‘Toyota is good, but we can be better’ and continuously strive for improvement in all areas.
Lean manufacturing allows manufacturers to be fast and nimble enough to quickly react to changes in customer demand and do it with little inventory. Companies can no longer stock large quantities of raw materials, accumulate work in process and finished goods. Those old ways are wasteful and customers are not well served. In these changed times, lean supply chain performance must be the goal of every manufacturer. Creating the lean supply chain by streamlining the business and production processes to significantly reduce cycle time, decrease inventories, lower costs, and increase customer service, has become the mandate for gaining competitive advantage.
People like to proclaim themselves to the elite league of lean manufacturing organisations. Many use terminologies and jargons without understanding the underlying philosophy. Some even tell me they have done lean before. But then why are they not able to do it in their current jobs? Many organisations implement some lean tool in isolation and like to think they belong there, but are far from that exalted company. One CEO even told me “I have read the book three times and yet I can’t do it.” This may be true with many. People buy up books on the subject, read them and try to copy the forms. What they don’t realise is that most books deal with the logic but not so much the philosophy and culture that is critical to lean. Also, that they are a different industry compared to the narration, their demand patterns are different and so are their varying volumes and variables. Toyota is a zaibatsu, most others are not. The ability to successfully transform your organisation from discrete to lean requires some things beyond the books that one read.
So, while so many crave to be in league with successful lean manufacturers, why do most fall short of being there? Why are there so few companies that have become successful at lean manufacturing in India? There can be many reasons and many explanations; here we will try to understand some that are critical to success:
Integrating key principles into daily behaviour
A common experience amongst all teachers and consultants who teach lean concepts is that even though they show the way, people are unable to duplicate it on their own, although they have understood it. The key principles of lean are very simple to understand, but difficult to integrate into daily managerial behaviour. It takes attitude and discipline. A Toyota Sensei (master teacher) once said, “I can show you how to do this, but you can’t do it.” What he actually meant was that one could get the idea intellectually, but to actually do it one would have to do a number of key things opposite to the way one had done them for years. One’s instinct and gut feeling would make it very hard to do the lean thing. It takes dedication, persistence, perseverance and staying focussed on the goal to achieve it. Changing habits is hard in the beginning, but only by inculcating new habits into one’s daily routine, one can build a lean culture.
For example, the idea of one-piece flow sounds straightforward. But do you have any administrative processes that actually operate in a one-piece-flow fashion? It’s easy to say ‘continuous improvement,’ but we think of making a step-by-step improvement. We don’t really believe that improvement can be continuous. We don’t actually believe that the whole point of a lean transformation should be to build a lean-learning culture, where continuous improvement is what is expected everyday – forever.
Coming from an organisation that was among the pioneers in the country to work on building a lean culture, transforming the organisation from group technology concept was a great learning experience. Changing layouts to adapt single piece flow saw throughput times come down from as high as 45–60 days to as low as 2–3 days or even less. Lean thinking had made the unattainable possible. The change took a lot of learning, teaching, training, doing, persevering, falling down, failing forward, getting up and improvising. The change was not always easy, but the results were always encouraging and inspiring. If only we had a Sensei guiding us then, our process would have been faster and better.
Learning from a Sensei
One question that I am asked frequently is, “If you knew back then in the early 1990s what you know now about lean manufacturing, what is it you would have done differently?” My answer is always the same; “I would have asked for a Sensei to learn from and assist us in our journey.”
To be successful you need great people and a system to support. Great people who can cultivate their success by working to develop highly dependable suppliers, working to develop specific technology and processes to benefit the company and collaborate with equipment suppliers to develop equipment that fits your company’s specific needs of your production system. A good Sensei will be invaluable to the process helping develop both the people and the processes. More importantly, assisting in building the right culture.
If the process is so simple as stated, then why so many fail or fall short of their potential achievement? The reason is mainly in the human nature. It is not possible to duplicate the success of any other company by merely imitating its techniques. In discussing techniques we forget the importance of relationship. Perhaps this may be the reason why many management fads fail. People imitate the technique organised elsewhere but fail to live in the fundamental state of leadership, as did the person who originated the technique. This is why we need Sensei who can assist in transforming the culture, and not merely make mechanical adjustments or apply some tools at random. The techniques are valuable, but people cannot learn to make them work if they are not challenged in the process of learning how to make them work. The dilemma is people want to merely copy the outward appearance of what Toyota is doing, but they do not want to pursue the much harder and time-consuming aspect of changing their own behaviour to replicate Toyota’s culture and the way it is set up.
When I was implementing the JIT techniques at MKL Hubli factory back in the early 1990s, I had to deal with my own limitations and face adversity as I moved ahead. At times I felt lonely and at times had the feeling as though I was walking naked into the land of uncertainty. Yet, I was able to do it because I had very strong beliefs in the needs and benefits of the system we were then evolving and developing. Curiosity kept me going forward, exploring, experimenting and opening new doors. There were hardly any known lean organisations in India then. The system requires capable people to maintain and continuously improve it. I would spend no less than about three to four hours everyday in training people at different levels. And I must add here, this valuable time put into training never diminished our output, but it actually improved our productivity. Merely installing the system without appropriate development of skills and abilities will produce limited benefits, and the primary purpose of the system itself – increase performance through increasing capability of people – will be lost. The concept is simple to understand but difficult to apply. It requires a dedication to personal change and a realisation that only through facing adversity and hardships will the true benefits be achieved. It is simple but not easy. I can now tell you that the feeling of loneliness was perhaps because I neither had a Sensei nor a lean thinking professional at the lateral end to bounce ideas, and so had to pave the path almost single handedly. You are lucky today, you can avoid making the same mistakes we made back then because today you can be assisted by an able Sensei.
There are very few master teachers (Senseis) out there. But most of your leadership lessons will come from attempting to start lean transformations. It takes time to learn lean tools at a fundamental level. We think of going to class to learn but the real learning is in doing it. Today’s organisations that want to build a lean culture can benefit by seeking to work with Senseis who have been there and done that. The basic learning element for TPS (Toyota Production System) is the weeklong Jishukin or voluntary study event. At MKL Hubli we called it a kaizen event or rapid continuous improvement (RCI) event. Of course, the ‘voluntary’ part was not in the same concept as probably TPS, but the goal was market leadership and we used lean manufacturing as our competitive strategy to build our competitive advantage. It worked very well. It is through these RCI events that everybody from manager to workmen learnt how to apply lean tools and concepts. And it’s only from a great deal of this kind of experience that you actually come to believe the core principles of lean manufacturing.
Based upon personal experience, I don’t expect someone to be a good Sensei at the tools level of knowledge without relevant experience and success under his belt of actually having led the transformation and built the lean culture preferably from the chair of a CEO. As students of lean, we always want to short cut this experience, and doing so never works. Because, at any point on the journey, ‘we don’t know what we don’t know.’ We won’t come to learn something, to believe something until we get there through personal experience.
At MKL in Hubli we had lean learning sessions every week for the managers and workmen. This approach is still the primary lean learning method. If your real goal is to build a long-term learning culture, you should keep in mind the learning value of every Jishukin or RCI event for the members of your organisation. It’s one hidden asset on your balance sheet that can really grow.
Leadership is critical to the success of your objective
“The successful person has the habit of doing the things failures don’t like to do. They don’t like doing them either necessarily. But their disliking is subordinated to the strength of their purpose.”
The achievement of your goal is assured the moment you commit yourself to it. A third way to answer the question of “why are there not more lean successes in India?” comes down to leadership. In business schools and other places we are trained to manage, rather than to lead. We are taught, for instance, that delegation is a skill you must use as a successful manager. And this statement is true in many ways – you can’t do everything and expect to manage a large organisation.
But it can be false in the lean setting if you are undertaking something that involves new levels of learning, and no one in your organisation has ever been there before. As a senior leader, you need to get some ‘learning,’ or you won’t have the minimal knowledge necessary to manage the lean transformation. In addition, something that is transformational by definition involves a lot of change management. You cannot delegate change management to someone who has not been there before, is lower in the hierarchy, and doesn’t have the clout needed to manage the politics of change. Given the magnitude of change, the team wants to know that the leader is also going there.
The all-important culture
Simply said, culture is what we do and how we do it. The leader always builds the culture. What and how we do is based on what and how we think. Lean thinking is a culture. It’s got to do with the thinking at the top. Lean will only succeed if the senior management believes in this changed thinking. One cannot expect the lower rung to adopt lean thinking while at the top one wants to go by their old cultural ways and thinking. There will be a clash, and you will not get your desired results.
Change is uncomfortable. Habits die hard. People don’t want to change and for a variety of reasons, mostly they don’t want to get out of their comfort zones. Resistances come up in the form of smoke screens, and we know their reasons are not the real reasons. Everyone likes to do what he likes and not what should be done. There are those who do not know how to deal with the change. Also when marketers make overstated commitments beyond the competence and capability of the manufacturing set up to meet commitments, it unlocks doors to potential failures and gives rise to frustration. At MKL, we had developed two tools to overcome such situation: one being the predictability tool and the other, the delivery tool. Both these were measured on a daily and weekly basis and continuously adjusted to balance the market demand with the intrinsic capacity to meet those demands and regulate the flow of material through the value stream.
Although lean is a different environment, philosophy and culture, one might wonder, ‘how safe is it to walk into this unfamiliar land? Can I do it? Are my people good enough? What will happen if we run into troubles? Will it slow me down? Will I lose production and sales? How long will it take?’ etc. As long as you have an able and competent Sensei by your side, you are not walking naked into any land of uncertainty. An able Sensei will be able to dovetail the appropriate programme for your organisation.
Lean manufacturing tools like using 5S programme to organise workplace will remove unneeded and obsolete inventory. Total productive maintenance will reduce machine downtime, and quick change-over allows for manufacturers and assemblers to respond quickly to changing customer demands. JIT techniques, and the use of Kanbans are simple lean tools to ensure a smooth flow of materials through manufacturing and assembly. Many companies around the world have used these techniques, and in India too, to identify and eliminate wasteful delays in the external and internal supply chain.
Right at the top
Why now? You may ask. After all the manufacturing is in boom. Why not now? There is an old saying that applies around the world, ‘If you continue to do what you have always done, you will continue to get what you have always got!’ Most Indian manufacturers are not satisfied with their current global, Asian or domestic, competitive position. If they stay on their present path they will get the same results they have always got. Lean manufacturing tools can help improve your processes all the way from order entry to delivery to the customer.
Whatever happened to USSR, East Germany, Czechoslovakia; they were said to be the ‘new’ civilization? Where are they now? Are Indians companies falling short of continuing good practices? Managing change or change management is the role at the top, one that cannot be delegated. Excellence can be attained if you risk more than what others think is safe, care more than what others think is wise, dream more than what others think is practical, and expect more than what others think is possible. The seed of lean thinking has to incubate right at the top.
Download the original PDF Leans-the-way.pdf
Download PDF ↓ Originally published in Search — The Industrial Sourcebook · September 2007
Keep reading
More on Lean Manufacturing
ARTICLE
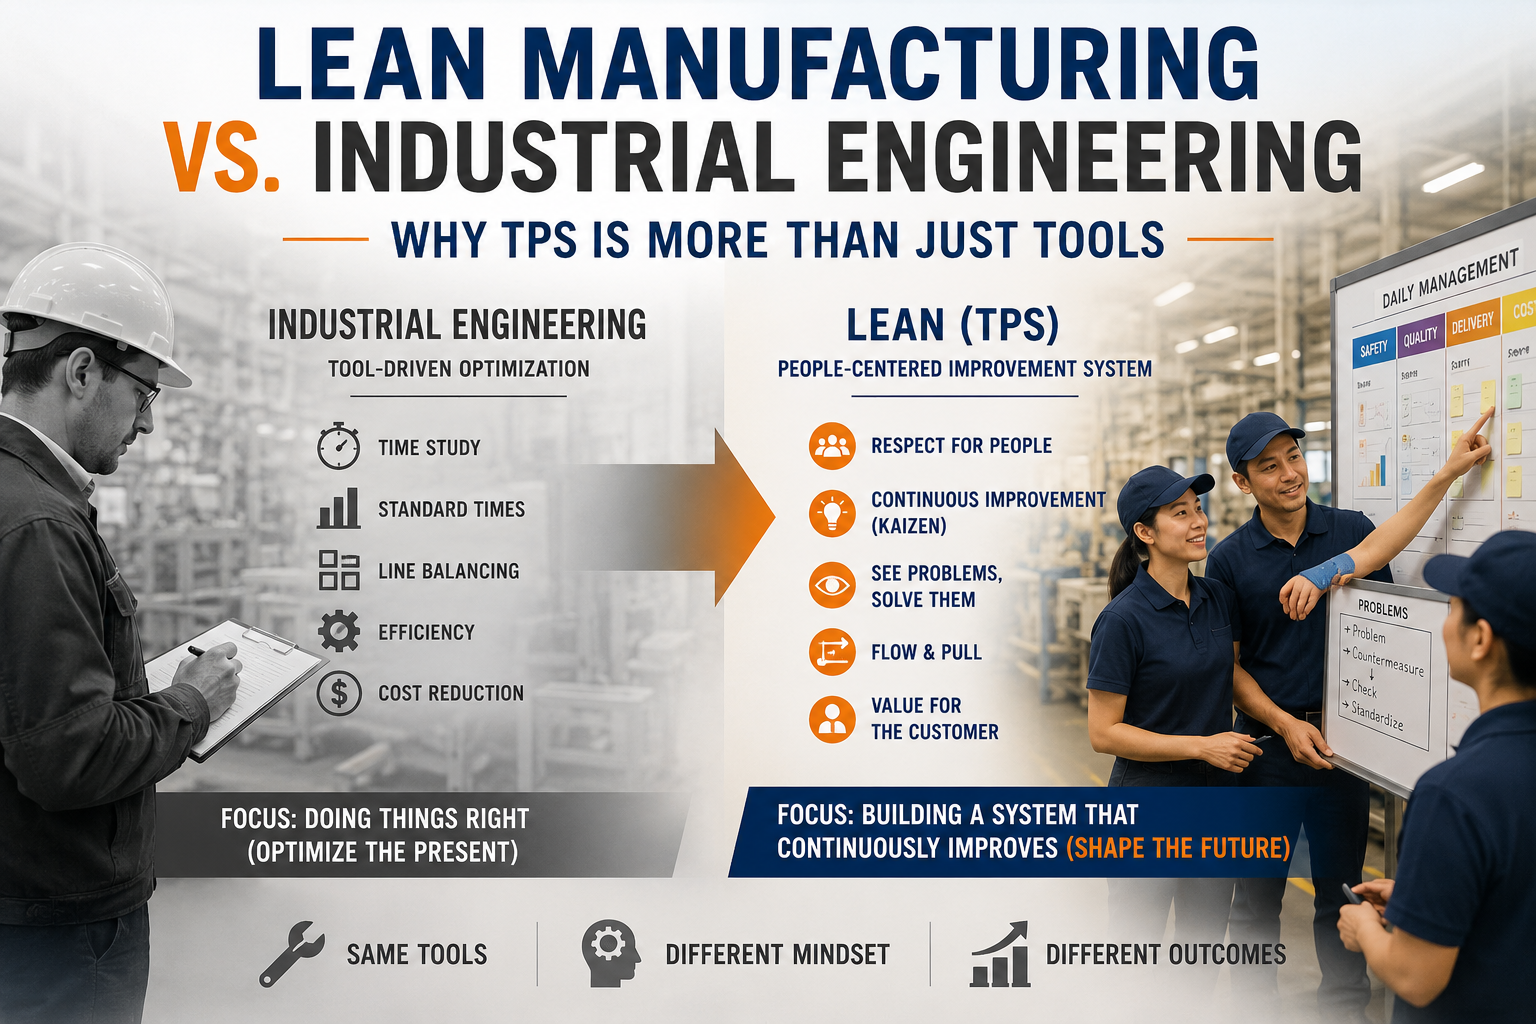
Lean Manufacturing vs. Industrial Engineering: Why TPS Is More Than a Toolkit
Lean ManufacturingMay 2026