PUBLICATION
The Lean Mindset
Thinking lean isn’t just about costs; it’s about customers. Once your manufacturing activity is centred around customer needs, quality follows automatically.
Being lean means not being obese – and that’s good for the health of the body. Everybody wants to be lean, but lean is often mistaken for thin. Thin is fine, but lean is actually about being healthy, agile, fit and alert. The real benefits of thinking lean come from the culture and discipline you build into your daily routine in five important areas – exercise, food and eating habits, positive mental attitude and rest, cutting out on alcohol and tobacco, and diet supplementation. These five aspects will determine your health and ability to lead a healthy life.
Like human beings, companies, too, are seeing the advantages of thinking lean. At a machine tool factory (MTF) that was among the first in this country to make an attempt to implement lean manufacturing, the management made a long-term decision to move away from the batch production system to the ‘pull’ system. The basic idea was to adopt lean thinking as a strategy to reduce costs and lead times, improve quality and provide better service to customers. The reason why this company’s experiences are worth sharing is simple. They discovered that “to change it all, we had to change nothing at all.” All that changed was the way they began to think. The important factors for success in lean manufacturing are focus, patience, long-term objectives and goals, an unfailing commitment to quality, and investment in people, manufacturing facilities and the products themselves.
The thinking culture that needs to be developed can be summarised as follows: “Do the right thing for the company, the customer, employees and society at large.” After the advent of the internet, the greatest change we have seen is how the markets have evolved and become customer-centric. It is very important for any company to align itself around satisfying the customer. At MTF, they developed a single common price for all customers – big or small. They ensured that no two customers paid different prices for the same product. To make this happen they developed nine governing principles that became operating policies. These were written down and signed by the CEO and handed over to each and every dealer. This created the right environment to do business the way it should be done. When they discovered defects they spared no efforts or costs to replace the parts or to rebuild the product (even if the product had to be brought back from Europe or America).
At MTF, the ultimate test of character was in the way they treated their customers – it’s like how you treat somebody who cannot fight back. In building trust with employees, they never let business decisions undermine trust and mutual respect. When they had to close the factory down because they had no orders, they invited the employees for a discussion and to explain a proposed strategy that could revive the business. This included paying employees a greater part of their salaries while they stayed at home and letting their engineers conduct the most intensive market survey in the history of the machine tool business – and possibly even in the history of the country. Paying the employees, letting them visit the factory and ask questions on the progress, and calling the required employees to build machines when orders were received during closure built confidence in them on the genuineness of a management that was committed to remain in business.
For a firm that had produced machines and supplied over 80 per cent of them to customers in America and West Europe, this change in the manufacturing strategy was a cultural revolution. Lean thinking involves the cultural transformation of an organisation. In the case of MTF, there were two major intents on the strategic blueprint. The first was to be able to produce and deliver products in small quantities, with short lead times, to meet specific customer needs, including day-to-day shifts in customer demand (JIT). The second was to have built-in quality in their products (jidoka).
MTF went about changing its culture using a systematic process. First, it put the customer ahead of everything. The managers spoke to over 10,000 of them, and analysed their needs using problem-solving tools such as Pareto and Dr Ishikawa’s Fish Bone Diagram. They realised that defining customer values is really the first key step to quality, delivery, cost and service. By monitoring demand, they developed a factual tool called the demand rate. This is like a moving bar and changes regularly – you define the period suitable to your customers and industry. This is a predictability tool that can be used to forecast the most likely trend.
Next, they defined the value stream. The demand value has to flow at a defined rate uniformly throughout the value chain – from the raw material processing stage (be it castings or forgings) to vendors and suppliers, and through the manufacturing cells and assembly lines to the customer. They made it flow by implementing another tool called the flow rate. This is in sequence to the demand rate and defines purchase ordering, pull quantities and the rate at which work-in-progress flows through the value chain. They now had authorised ordering material based on a firm customer order. So they were actually pulling from the customer backward. This ensured that there was no pile-up of inventory. By working on a culture of reducing time, from the time a customer order came in to the point of collecting payments, they were actually striving for excellence.
The right process will always produce the right results. In a one-piece flow, if some production problem occurs, the whole line stops. So this is a demanding discipline that many shy away from. But, on the other side, when production stops, everybody is forced to solve the problem and eliminate it – continuous improvement. This builds better teamwork and also makes the team members grow. They realise that shortening the time gap between raw material and finished goods will lead to better quality, lower the cost and shorten delivery times. This flow also induces other improvements, such as built-in quality, productive maintenance, etc.
Exposing problems
The lean expression is like lowering the ‘water level’ of inventory, exposing the problems (like rocks in the water) and removing them – or if not, sinking with them. (Can you guess why people are often afraid to expose problems?) Traditional processes tend to take days or weeks to complete the process, while lean thinking can accomplish the same in much lesser time. At MTF, for example, a spindle used to take about six weeks to complete – with waiting stations at many places, and frequent rerouting. The component also travelled a few kilometers of distance in the process. After implementing a cellular layout and flow concept the part was not only completed in three days but was of far better quality too.
In their attempt to eliminate all waste, they looked at areas such as over-production, waiting for man or machine or any consumable, unwanted movement of materials or men, elimination of unwanted operations (overprocessing) and incorrect processing, unnecessary inventory (unauthorised) or defects of any kind. Much of this became possible by harnessing unused employee creativity. They reduced overproduction by strictly adhering to the ‘pull quantities’ which were reduced every time they achieved lead-time reduction. Multi-skilling their operators, they eliminated any process waiting for anyone. The only time any component waited for a machine was in case of a breakdown, but most of the times their breakdown times were less than one half of one per cent of total available time.
By relaying the manufacturing lines as and when an improved process was discovered, and by using the flow concept, they were able to eliminate unwanted movement and non-value adding processes. At MTF, “flow” meant that whenever a customer placed the order, it would automatically trigger the process of ordering the raw material. When there was only one customer order, “flow” meant the processing of a single piece. This was a mindset achievement. The benefits they realised were manifold: their quality improved dramatically and saved a lot of money, some of which they passed on to the customer. They became very flexible and were able to change over models in a small turnaround time. Their productivity almost doubled in a short time. It happened even as the manpower numbers went down gradually by over 20 per cent. They were able to free up one complete hangar – almost one-third of the floor space – and use it for expansion and developing new products.
The management reorganised the entire factory into ‘lean manufacturing cells’ by continuously changing the layouts many times, creating continuous process flow and bringing problems to the surface. The newly structured ‘cellular manufacturing’ adopted the ‘pull system’ to avoid overproduction and implemented the single piece flow concept. The cells popularly used a straight line or ‘U’ layout, with almost all operators multi-skilled and able to operate a minimum of three machines based on the one-up-one-down concept. The employees were empowered to stop the process if it produced rejects. Quality circles within the cells became active at solving problems and resolving bottlenecks. The one thing they passionately did was to build a culture focusing on the root cause of a problem and eliminating it. This built organisational learning.
Productivity
The workload was almost levelled out. Productivity improvement came from eliminating all non-value adding processes, reducing all types of downtime on the machines and assembly stations and improving and re-engineering the processes. Components that earlier traveled kilometres now had to travel only a few dozen metres for machining to be completed. A machine was allowed to stop producing parts once the required rate of flow was achieved. To level out the flow of finished goods, stocking was authorised at the rate of one week’s flow or output. This translated itself into kanbans of proportional time sizes at critical stages. This, they found, was better to start with rather than produce against a daily fluctuating demand.
MTF also brought in equipment additions to substitute dependent labour. They changed their focus from keeping the operator busy to producing against the actual demand. They simplified the whole system by not keeping information in computers but by transferring it onto the shopfloor through a visual signalling system under the eyeball control of employees. No problem ever remained hidden.
They found that by keeping lead times short and focusing on keeping production lines flexible, they actually got higher quality, better customer responsiveness, better productivity and better utilisation of space and equipment. Using the tools of continuous improvement and by re-engineering the processes, they released one-third of the total floor area to house new assembly lines of CNC machines and co-branded products. Their best machine upkeep time was generally above 98.5 per cent. Focusing on quality rather than cost actually brought down the costs; coupled with rationalisation and re-engineering, they actually passed on huge price benefits to customers.
In the days when MTF produced to the push system, they had seen customer demand change many times. This had often left them with unused inventory. A very ideal form of one-piece flow is very hard to achieve. So to balance the pull, cycle time and inventory, they built kanbans for managing and ensuring the flow and production of material in a just-in-time production system using simple visual signal cards and bins. As orders came in from customers, they created a levelled schedule through a ‘flow rate’. That flow rate was used to define the size of assembly stations and size of kanbans, apart from order quantities on the purchase orders. The batch size on the signal cards automatically changed with the change in flow rate. They had defined the trigger point for reordering from each kanban or bin.
In their experience, they had learnt that customers do not buy products in a predictable manner. The push system runs the risk of building an inventory of unsold goods. The resources on hand will not be effectively and optimally used. This builds uneven demand and pressure on upstream processes. MTF worked on levelling the flow so that they could make what the customer wanted and when he wanted it. This reduced or minimised the risk of having unsold goods. It allowed optimal use of labour and machines and evened the demand on the plant’s suppliers and upstream processes. The best place to see how a schedule is levelled would be at a Toyota factory.
MTF’s success largely stemmed from the cultural change the organisation underwent. The principle they adopted – of stopping the process in case it was producing defects – was intended to get the quality right the first time. In the beginning it created havoc. But they had seen worse – a very high rate of defects, with machines even being recalled owing to defects and customer complaints. With low levels of inventory and short lead times, lean manufacturing dramatically increases the importance of building right the first time. This is the jidoka philosophy – build in quality. At MTF they worked intensely on problem solving, error proofing, and training people on the shopfloor to actively participate in quality circles, 5S, et al. They standardised to the maximum possible extent and kept doing this in their processes, documentation, designs, methods, and actions. One could say their social structure changed from a coercive one to an enabling structure.
In their efforts to simplify processes and make them easy to control, they used the visual or eyeball control technique. Defects and action plans for improvement were boldly displayed in the respective work areas – shopfloor or departments. Graphs displayed the present situation, and improvement implementation plans showed the future trend. Keeping it visual and empowering people enabled operators to better control the processes. Demonstrating their belief in growing their own leaders, an internal candidate was picked to head the business. When the factory was re-engineered, the managers were allocated new jobs utilising their competencies to the hilt.
At MTF, the customer always came first. People were treated as the company’s most important assets, and the management strongly believed that while machinery depreciates, people appreciate in value. For exceptional results you must develop exceptional people or leadership. The result of developing exceptional people and teams produced remarkable and substantial growth results at MTF rapidly.
One of the key reasons for MTF’s success was the respect with which they treated their customers, partners and suppliers. They helped their dealers and suppliers improve and become more effective. Dealers were constantly trained, given written down policy guidelines, and treated as the most important persons on the premises. Suppliers were identified and not only trained on the philosophies now used in-house, but their shopfloors were reorganised and relaid with the pull concept. Some solid suppliers were upgraded to tier one to supply assemblies. The philosophies imbibed in this process also helped save some sick suppliers.
Lean manufacturing is about the culture of developing people, suppliers and partners who can reduce lead times everywhere. By raising the bar on developmental lead times for new machines, MTF left behind a new benchmark. A whole new range of machines was developed from concept to finish and displayed in less than a hundred days using concurrent engineering and developmental techniques. In three months they had changed their entire portfolio of products. This came about following the closure of the factory when orders dried up. Such unique turnarounds can only happen with consistency of leadership and philosophy.
Strategic culture
Lean manufacturing is as much a strategic culture as it is a manufacturing strategy. That’s why it always starts at the top – literally and figuratively. “You can stop the invasion of an army but you cannot stop an idea whose time has come,” wrote Victor Hugo. That idea is ‘lean manufacturing’. Its time has come, if you want to accelerate growth, profitability and customer share. Lean is about working smart and as a culture can be adapted to any business, be it manufacturing, trading, IT, ITES or service industries. If you want to be Toyota tomorrow, you have to begin thinking lean today.
Benefits of lean thinking at MTF
Relentless reflection and continuous improvements dramatically improved MTF’s business processes, eliminating wasted time and resources, building quality into workplace systems, finding low-cost reliable solutions to expensive technology, perfecting business processes and building a learning culture for continuous improvement. The following are the benefits MTF obtained over a three-year period by implementing “lean manufacturing.”
| After implementing ‘lean’ | Before implementing ‘lean’ | |
|---|---|---|
| Lead times (products) | 5-7 days | 45 days |
| Lead times (major components) | 2-7 days | 30-60 days |
| Quality index (rejects & non-conformance levels) | 0.3 % (close to 5 Sigma) | 20 % |
| Customer satisfaction | 96 % | 44 % |
| Inventory turns | 11.5 | 1.45 |
| Products | 8 | 2 |
| Models | 27 | 7 |
| Domestic dealers | 54 | 12 |
| International dealers | 18 | 2 |
| Manpower | 640 | 840 |
| Turnover | + 496 % | - |
| Profits | + 15 % | - |
| Cost reduction to customers | 22-29 % | - |
Download the original PDF The-Lean-Mindset.pdf
Download PDF ↓ Originally published in Indian Management · November 2004
Keep reading
More on Lean Manufacturing
ARTICLE
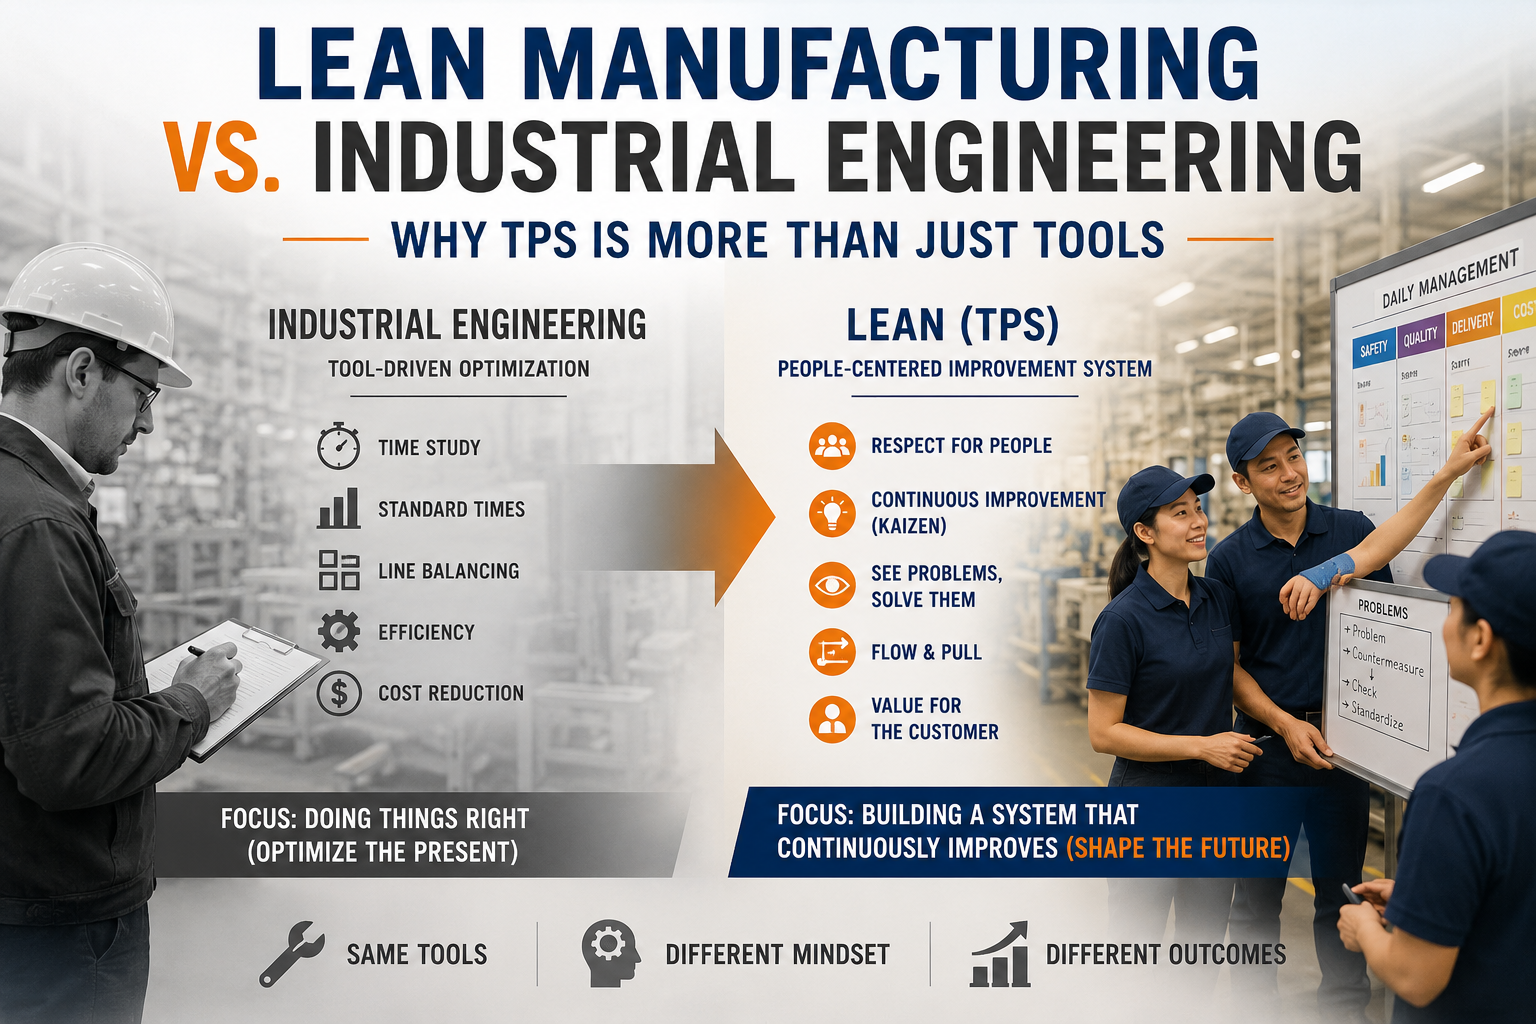
Lean Manufacturing vs. Industrial Engineering: Why TPS Is More Than a Toolkit
Lean ManufacturingMay 2026